China Shredder: A Practical Guide to Types and Performance
2026-09-19
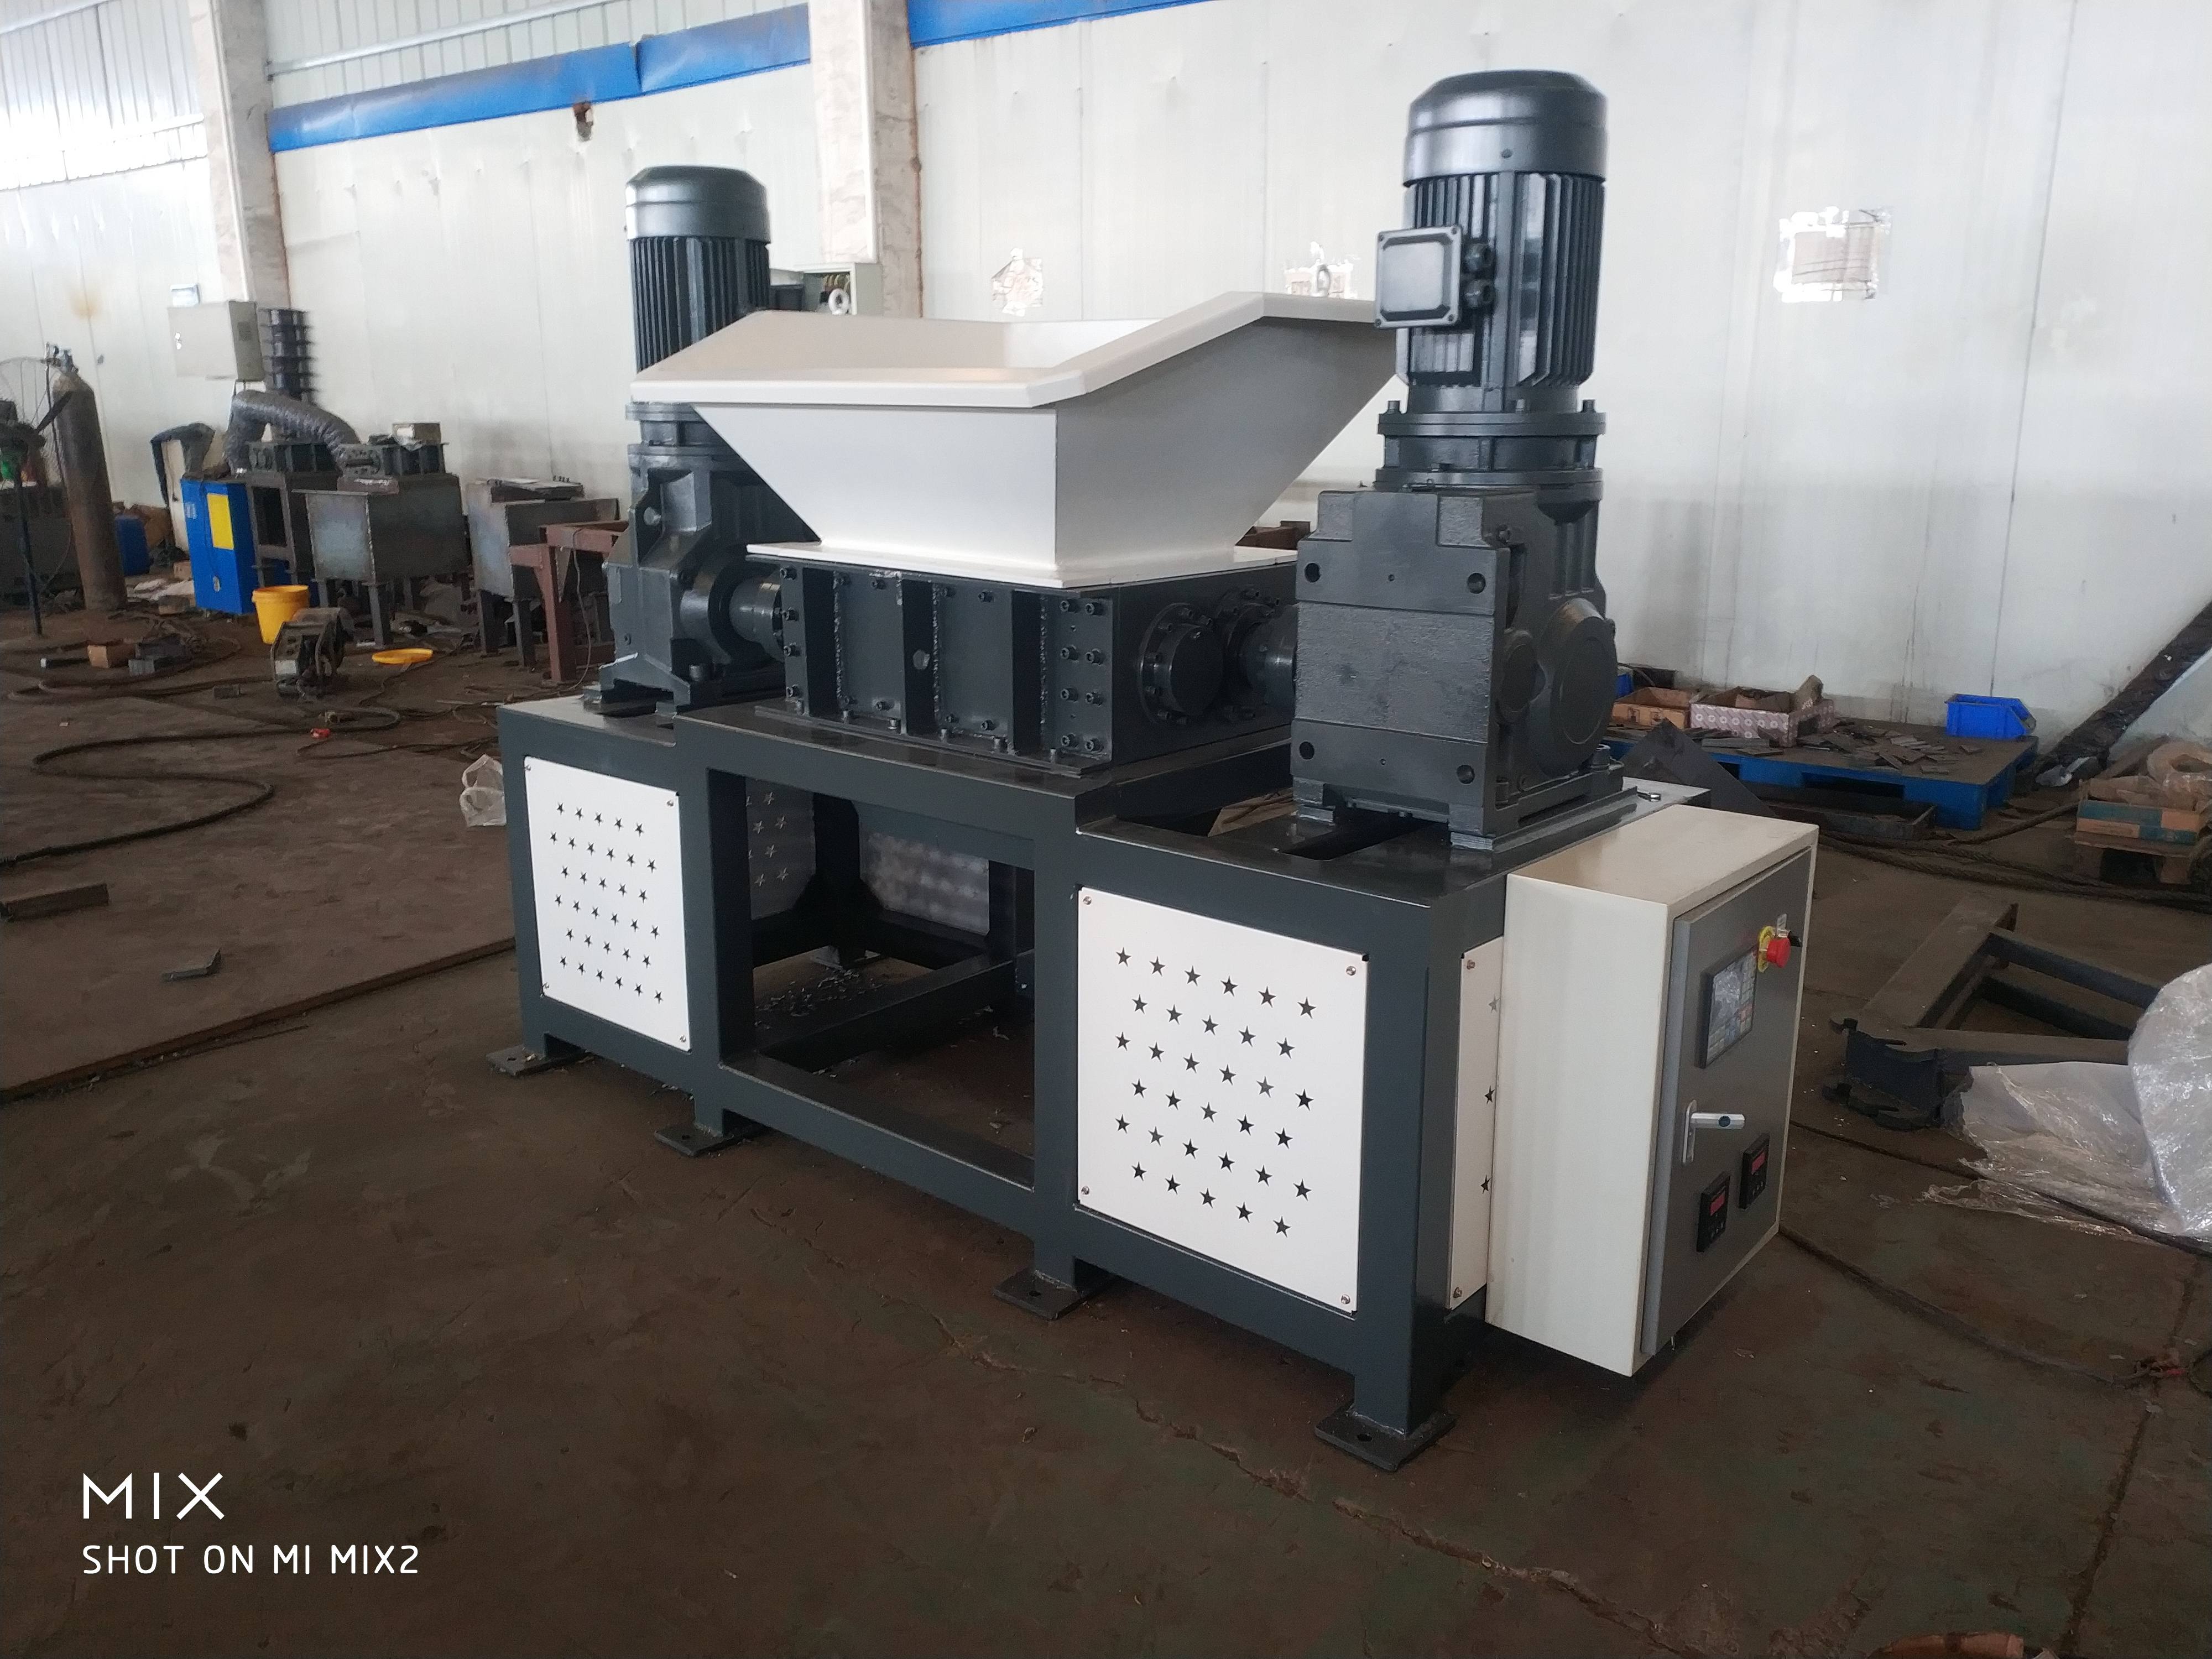
Choosing the right industrial shredder in China often means wading through conflicting specs and marketing claims. From single-shaft to quad-shaft designs, each type promises high performance—but what actually holds up under real material loads? This guide strips away the hype, breaking down key shredder types and the performance metrics that matter most. You’ll also see why Shengzhong Shredder has earned a reputation for units that deliver consistent throughput and durability without surprises.
The Core Families: Single-Shaft, Double-Shaft, and Beyond
Single-shaft designs are the workhorses of the rotary engine world. They tuck the crankshaft, rotor, and output shaft onto one common axis, which keeps the whole assembly compact and surprisingly simple to manufacture. This layout works well in applications where space is tight and torque demand stays moderate, but it does force the intake and exhaust ports into tighter corners, which can slightly choke breathing at high rpm.
Double-shaft configurations split the load between two parallel shafts, typically a main crank and a separate output shaft geared together. That extra shaft lets engineers place ports more freely and balance combustion forces more evenly. The result is smoother operation at higher speeds and better thermal distribution, though the added gearing and bearings push up complexity, cost, and weight. Most performance-oriented rotary engines settle here after weighing those trade-offs.
Beyond these two core families, a few experimental layouts branch out—triple-shaft arrangements, offset rotors, or hybrid piston-rotary designs. These tend to chase specific goals like reduced vibration, variable compression, or multi-fuel capability. They rarely make it past prototype stages, but each one quietly influences how mainstream rotary engines evolve, borrowing a port shape here or a bearing layout there.
Throughput and Power: What the Numbers Actually Tell You
Throughput and power ratings are often treated as the definitive measure of a device's capability, but the relationship between the two is far more nuanced than a single spec sheet suggests. Throughput, typically expressed in bits per second, indicates how much data can be moved in a given window. Power, measured in watts, tells you the energy cost of that movement. However, these numbers are not static. They shift with distance, interference, packet size, and even thermal conditions. A system that posts high throughput on a lab bench may struggle in a noisy environment, while a lower-power design can actually sustain better real-world throughput if it avoids throttling or retransmission storms. In other words, the headline figures rarely reveal the true operational envelope.
The more meaningful metric is often efficiency: how many bits you can push per watt. This ratio becomes critical in battery-operated devices, dense mesh networks, or any deployment where heat and energy budgets are constrained. A device that achieves 80% of the peak throughput at 50% of the power draw may be a far better engineering choice than one that hits the maximum data rate only briefly before hitting thermal limits. Yet many buyers focus solely on the top-line number, ignoring that sustained throughput under realistic load is what actually determines user experience. Manufacturers sometimes exploit this by quoting burst rates that cannot be maintained for more than a few seconds.
To truly understand what the numbers tell you, you need to ask under what conditions they were measured. Was the throughput figure achieved with a single client in an isolated chamber, or with dozens of devices competing for airtime? Was the power draw measured at peak, average, or idle? Does the chipset dynamically adjust voltage and frequency to trade performance for thermals? These questions matter more than the raw figures. A system that gracefully degrades throughput while keeping power consumption flat is often more predictable and reliable than one that swings wildly between maximum performance and forced shutdown. In the end, the numbers only tell you the boundaries of possibility. How the system behaves between those boundaries is where the real engineering lives.
Material Matters: Matching Blades to Plastics, Wood, or Metal
Plastics require a different approach because they can melt or chip. A blade with a high tooth count and shallow gullets keeps heat down. For acrylic or polycarbonate, a triple-chip grind or a dedicated plastic-cutting blade prevents chipping; slowing the saw and clearing chips helps avoid rewelding. If you're using a jigsaw, pick a blade with a fine tooth pattern and keep the orbital action low or off.
Wood blades split into two camps: ripping and crosscutting. A ripping blade has fewer, deeper teeth for fast cuts along the grain, while a crosscut blade has more teeth for clean edges across the grain. Combination blades work for general use but compromise on both. Hardwoods need a blade with more teeth and possibly a stabilizer to reduce vibration.
Metal cutting demands slower speeds and blades made for the job. Bi-metal and carbide-tipped blades hold up longer, but the real key is matching TPI to material thickness—thin metal needs high TPI (around 24 or more), thick stock needs lower TPI so chips can clear. Use light feed pressure, and add cutting fluid whenever possible; dry cutting overheats the blade and work-hardens stainless steel.
Built to Last: Maintenance Habits That Extend Shredder Life
Most shredders die young because owners treat them like disposable office supplies. The single most impactful habit is oiling the cutting head before the motor starts to strain — a few passes of shredder oil across a sheet of paper, run through in reverse, keeps blades from gumming up with paper dust and adhesive residue.
Overfeeding is the silent killer. Instead of forcing the maximum sheet count, feed about 75% of the rated capacity and let the machine finish its cycle before adding more. If the shredder starts to labor or the sound changes pitch, stop and let it cool down for at least fifteen minutes. Heat is what warps the plastic gears and shortens motor life far more than actual cutting wear.
Finally, get into a weekly rhythm of clearing the teeth with a dry brush or compressed air, and empty the bin before it's completely full — packed confetti forces the cutters to work against their own waste. These aren't chores; they're cheap insurance that turns a mid-range shredder into a ten-year workhorse.
The Real Cost: Beyond the Purchase Price
The sticker price is rarely the number that ends up mattering. A laptop that costs $899 might seem like a bargain until you add the case, the dongles, the extended warranty, and the software subscriptions that keep it useful. Those quiet add-ons slip onto the receipt before you even leave the store, turning a so-called deal into a full-price purchase with extra steps.
Then there's the ongoing drain that never shows up in the checkout total. Energy consumption, replacement parts, compatibility upgrades, or the hours spent troubleshooting a product that wasn't designed to last all quietly eat away at your wallet long after the initial excitement fades. A cheap printer, for instance, can become one of the most expensive things in your home office once you factor in ink cartridges that seem to evaporate.
Savvy buyers have learned to ask a different question: not how much it costs today, but how much it will cost over the next three years. That shift in thinking exposes the true price of ownership, and it's often the reason a slightly higher upfront expense turns out to be the cheaper, saner choice.
From Recycling Lines to Medical Waste: Picking the Right Fit
Sorting equipment built for a recycling line rarely survives contact with red-bag waste. The physical demands look similar on paper—conveyors, shredders, separation—but the material behavior, contamination risks, and regulatory pressure are entirely different worlds. A star screen that happily tumbles PET bottles will jam on gauze and tubing within an hour, while an autoclave sized for municipal mixed waste would be overkill for a clinic's daily sharps load. The real question isn't which machine is “best,” but which failure mode you can live with.
Start with the operator's boots on the ground, not the spec sheet. Recycling plants optimize for throughput and purity; a hospital waste handler thinks about lockable hoppers, leak-proof seals, and whether the next bag might hide a needle. Medical waste lines need washdown surfaces that tolerate bleach, bearings that shrug off saline corrosion, and discharge chutes that don't trap infectious aerosols. None of those features appear in a typical MRF brochure. If the vendor can't explain how their shredder handles blood-soaked cotton versus wet cardboard, keep walking.
A smaller, simpler machine you can actually maintain beats a flagship unit that sits idle waiting for a technician. That holds double for rural clinics or mobile treatment units where spare parts might be a week away. Look for modular designs where one failed blade doesn't shut down the whole line, and question any sales pitch that lumps “general solid waste” and “regulated medical waste” into the same flow chart. The fit isn't about capacity numbers—it's about whether the operator can safely clear a jam at 2 a.m. without compromising the room next door.
FAQ
Single-shaft, double-shaft, and four-shaft models account for most domestic production. Single-shaft machines handle uniform plastics, wood, and paper well when consistent particle size is the goal. Double-shaft units are the practical choice for mixed or metal-bearing waste like e-scrap and tires because they tear rather than cut. Four-shaft designs cost more but add a secondary sizing stage, which helps when contaminants would otherwise jam a simpler machine.
It is usually the biggest factor. Reputable plants often use tool steels like D2 or DC53, heat treated to around HRC 58-62, because that balances wear resistance and impact toughness. Cheaper models may use low-alloy steel that dulls quickly on abrasive materials. Ask for the exact steel grade and heat treatment, not just a vague claim about 'alloy blades'.
Inspect the frame thickness, bearing brands, rotor concentricity, motor winding material, and control components. Welds should be even with no undercut, and the frame should show signs of stress relief. Adjustable blade clearance is especially important; fixed clearance machines get harder to keep in tolerance as parts wear.
Yes, but only if you select a low-speed, high-torque twin-shaft model with reinforced blades and a wear-resistant overlay. High metal content also calls for magnetic separation and a sizing screen. Running metal through a plastic-focused single-shaft machine will quickly chip or break the cutters.
Rotor diameter, blade count and arrangement, screen size, and feed method all play a role. At equal power, a large-diameter rotor provides more inertia but lower speed, which suits heavy loads. A small-diameter high-speed rotor works better on light materials. Actual output also drops sharply if the operator feeds material intermittently instead of keeping the hopper loaded.
Most offer distinct tiers. Economy models use domestic motors and standard bearings and work best in light-duty recycling. Mid-range and high-end builds often include Siemens or ABB motors, SKF bearings, and PLC controls. Many export machines use a modular design so common wear parts can be sourced easily, which lowers long-term service costs.
Daily cleaning of the cutting chamber and screen is a must, along with checking blade bolts. Weekly bearing greasing helps, but over-greasing damages seals. Monthly belt tension and electrical connection checks prevent sudden failures. Blades should be inspected quarterly and rotated or replaced when output quality drops. In very dusty sites, clean the electrical cabinet filters more often.
It usually is. Many suppliers offer PLC upgrades that use current feedback to adjust the ram or conveyor speed and prevent overloads. The main requirement is that the feed system can accept variable-frequency control; if not, adding sensors and a small retrofit kit often closes the gap. The cost is normally far below buying a new machine, and it improves both throughput stability and operator safety.
Conclusion
Chinese shredder manufacturers rarely compete on horsepower alone. The practical split starts with rotor architecture: single-shaft units favor controlled, uniform output for film and rigid plastics, while double-shaft machines bite through bulky wood, pallets, or metal drums with slower torque-heavy cuts. Beyond those two families, you will find specialty granulators and four-shaft refiners that exist less for raw capacity than for particle consistency. Reading throughput and power specs side by side matters more than chasing the highest kilowatt figure, because a high-speed single-shaft can choke on mixed waste that a low-rpm twin-shaft chews through without stalling. Blade material and hook geometry then decide whether the same frame handles HDPE, demolition timber, or light-gauge aluminum without premature edge rounding.
What keeps these machines running is rarely the motor; it is screen changes, rotor bearing checks, and knife gap adjustments done before vibration becomes visible. Buyers who ignore those habits end up paying far more in downtime and blade replacement than the initial price difference between a mid-tier and premium unit. The real cost calculation should include energy per ton, wear-part lead times, and whether the hopper design actually accepts your bulkiest input without manual pre-cutting. From dense recycling lines that need steady output to medical waste streams where containment and low dust matter as much as particle size, the right fit emerges only after matching cutter style, speed, and maintenance access to the specific material stream in front of you.
Contact Us
Contact Person: Leon
Email: [email protected]
Tel/WhatsApp: 8615385558866
Website: https://www.shred-waste.com