Cold Forged Parts Supplier Checklist Every Procurement Team Should Use
2026-11-18
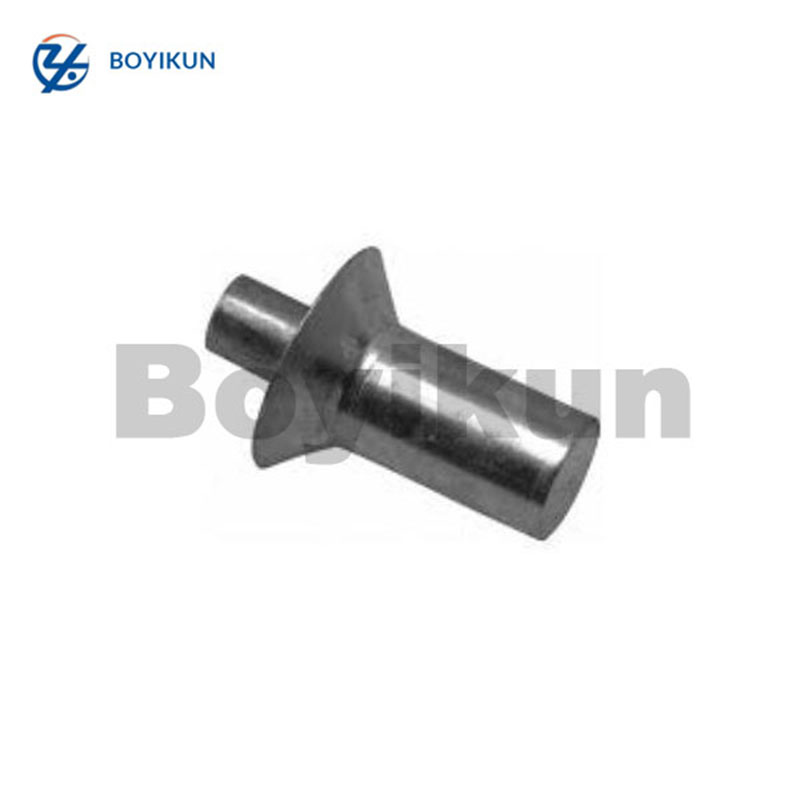
Cold forged parts rarely fail because of a bad drawing—they fail because a supplier looked capable in a sales deck and different on the shop floor. Procurement teams need more than a price comparison; they need a checklist that exposes how a forge actually controls material, tolerances, and lead times. BOYIKUN helps teams turn that checklist into a practical screen before a PO goes out. Here’s what to verify so your next cold forging supplier doesn’t just pass the interview, but holds up in production.
Trace the Steel Before You Talk Unit Cost
Talking about unit cost before you know exactly how the steel moves through your shop is like negotiating rent on a building you've never walked through. You can quote numbers all day, but they won't hold up once the first coil hits the slitter. Start by following a single order from receiving to shipping. Watch where the material waits, which operators handle it twice, and what gets reworked without being recorded. Those quiet minutes and extra touches are where the real cost hides.
Once you've mapped the actual path, you'll notice patterns that a spreadsheet never shows. A job that looks profitable on paper might travel across the floor three times before it's packed. Another might sit for two days waiting on a shared shear. Instead of averaging these delays into a generic overhead rate, pin them to specific steps. That lets you see which operations carry the real burden, and which ones simply look expensive because the steel took a bad route.
Only after this kind of tracing does a unit cost conversation make sense. At that point, you're not guessing or borrowing an industry benchmark. You're pricing from the way your own floor actually behaves. The number becomes easier to defend, and easier to improve, because you know exactly which turn in the flow is driving it up.
Read the Tooling Repair Log Like a Service History
A tooling repair log often reads like a cryptic list of dates and part numbers. But flip through it the way you would a used car's service history and the story starts to emerge. Look for patterns: repeated bearing swaps, recurring electrical faults, or a spindle rebuild every eighteen months. Those aren't isolated fixes—they're hints about how hard the machine has been pushed and where the next failure is likely to land.
Pay attention to what's missing as much as what's recorded. A gap of two years with no entries might mean the tool sat idle, or it might mean someone stopped logging repairs because the downtime got embarrassing. Notes like "customer complaint: vibration" followed by a wheel balance tell you the operator's patience is wearing thin. When you read between the lines, the log becomes a negotiation tool: you can walk away from a machine that's been nursed along with stopgap fixes, or you can budget for the overhaul that's already overdue.
Match Capability Studies to the Dimensions That Actually Fail
Most capability study schedules are built from the drawing, not from how the process actually behaves. That leaves a lot of dimensions in the monthly Cpk report that have not come close to a tolerance limit in years, while the few dimensions that regularly cause assembly trouble or customer complaints get buried in the same routine. Matching the studies to real failures means treating the capability plan as a ranking tool rather than a checklist that gives every dimension equal weight.
Start with the records that already exist: nonconformance logs, rework counts, field returns, and the dimensions that sit uncomfortably close to a limit. Those are the ones that deserve tighter sampling and a more serious capability requirement. Dimensions that never drift toward the control limits can be sampled less often or dropped from the routine study altogether, and those resources can move to where the process actually breaks down.
When the studies line up with the failures that matter, the improvement conversation gets sharper. Instead of staring at a long list of healthy green metrics, the team works around a short list of unstable or marginal dimensions. That makes the data more likely to lead to a real mold adjustment, a tool change, or a revised process parameter, rather than another report that simply gets filed.
Run a Live Containment Drill Before You Need One
The moment a breach actually happens is the worst possible time to discover that your team doesn't know who owns the database server or that the network segmentation you assumed existed was never fully configured. A live containment drill changes that. Pick a realistic scenario, maybe a compromised workstation or a cloud credential leak, and have the on-call responders walk through the exact steps they would take: isolating the host, revoking tokens, snapshotting memory, and notifying the right people. Don't script it heavily and don't stop when someone says "we would probably do this." Force the action to happen in real time, against a staging environment if possible, or at least against a clearly labeled test asset. The friction that shows up is exactly what you're there to find.
Drills often fail in two predictable ways: they're treated as tabletop discussions where nobody touches a keyboard, or they're run so rigidly that every step is known in advance. Neither gives you much. Instead, introduce a small surprise mid-drill, such as the SOC losing access to the ticketing system or a key responder being unavailable. See whether the remaining people can still contain the incident without that crutch. Also time the critical first fifteen minutes. If it takes nine minutes to locate the right runbook or remember how to quarantine a container in your orchestration platform, that delay will be painful during a real event. Write down every pause, every wrong assumption, and every missing permission, then turn those into concrete fixes before you close the loop.
One less obvious benefit of a live drill is that it teaches people how to communicate under pressure. Panic tends to produce vague updates like "something is wrong" or a flood of irrelevant screenshots in a shared channel. During the drill, insist on clear status lines: what is contained, what is still unknown, and what is needed next. If the team can do that smoothly when the stakes are pretend, they'll have a much better chance of doing it when the stakes are real. Run the drill on a regular cadence, not just once a year, and change the scenario each time so you don't end up perfecting a single predictable play while leaving other gaps wide open.
Ask What Was Scrapped Last Quarter and Who Caught It
Most teams only review what shipped. The harder question is what got dropped along the way and who first called it out. Those cuts rarely make the highlight reel, but they usually carry more signal than the wins. A promising integration that quietly disappeared, a beta feature postponed without a note, a client request that kept slipping: each one points to a decision someone made or avoided.
Chasing the second half of the question changes the room. When you ask who caught the problem, you learn which people are actually reading the logs, testing the edge cases, or listening to customers instead of nodding through demos. That person might not have a senior title, but their early flag probably saved the team from a much worse quarter. Make their role visible and let them teach the habit.
This works best when it stays curious rather than punitive. If scrapped work gets treated as a secret or a failure, nobody will admit what was cut. But if you treat it as evidence of good judgment, the next quarter starts with a clearer sense of what deserves attention. You may also notice that some things were scrapped by default, not by decision, which is another problem altogether.
Lock Secondary Finishing Rules Before Sampling Starts
Secondary finishing has a way of becoming the last-minute variable. A drawing may specify the machined dimensions in full detail, but if the anodizing shade, grain direction, edge break, or sealing method is still open when samples are ordered, the supplier will choose whatever is cheapest or most familiar. Locking these rules early keeps the first article from becoming a test of everyone's assumptions.
A marked-up photo or 3D view tends to work better than another list in the purchase order. Highlight the surfaces that must stay raw, circle the edges that get a uniform break, and attach a physical or digital finish chip with the acceptable range. This removes vague language—words such as uniform, clean, or smooth, which mean different things to different workshops.
After the rules are fixed, do not let a minor sample issue trigger a quiet rule change. If a finish looks slightly different from the reference chip, check lighting, batch mix, and handling before rewriting the spec. Changing a finish rule mid-sample usually invalidates the very thing the sample was meant to prove.
FAQ
Start with whether the supplier has actually produced parts in the same material family and size range you need. Ask for a list of previous jobs with similar geometries, tolerances, and annual volumes. If their sample parts are mostly simple fasteners but you need complex safety-critical components, that gap will show up later in tooling and quality.
Request drawings and photos of tooling from past projects, and ask how they handle die wear, coating choices, and tool life predictions. A capable supplier will be able to explain why they selected a particular tool steel or surface treatment for a given part, not just send a brochure.
IATF 16949 is relevant because it pushes process control and traceability further than generic ISO 9001. Also look for documented PPAP practices, in-process dimensional checks, and a clear nonconformance process. Certificates alone should not override evidence of how they handle a rejected batch.
Break the quote into tooling amortization, unit price at different volumes, scrap allowance, and secondary operations. One supplier may quote a lower unit price but recover cost through fragile tooling and higher scrap. Ask them to explain their assumptions for tool life, cycle time, and material yield.
Watch for vague answers about current machine utilization, reliance on one shift, or lead times that shift every time you ask. Strong suppliers can show planned maintenance windows, backup tooling, and how they schedule repeat orders. If they cannot tell you when a specific press would be available, assume your order will not be prioritized.
No. Certificates confirm what the mill supplied, but they do not tell you how the supplier stores, cuts, heats, or traces material through their shop. Ask for a material flow example from receiving to final shipment, including how they prevent mixed heats and how they label work-in-process.
Check lubricant and phosphate handling, because cold forging depends heavily on surface preparation and coating quality. Also look at how dies are stored and maintained, how dimensional data is recorded during long runs, and whether operators can stop a job without management approval when something drifts.
Conclusion
Procurement teams often treat cold forged parts as a commodity and jump straight to price per piece. That skips the harder questions. Before any unit cost discussion, ask where the steel came from and whether the mill certificates match the heat lot, because substitution can hide in the supply chain. Then ask to see the tooling repair log, not a summary. Repeated die repairs on the same station usually point to poor process control or worn equipment that will show up as variation later. Capability studies only matter if they cover the dimensions that actually fail in your assembly; a Cpk on an easy outside diameter tells you little about a tight hole location or a critical radius.
A useful supplier check also includes a live containment drill. Instead of accepting a written procedure, hand the supplier a fake lot number and a suspect defect and see how quickly they can quarantine, trace, and report. Ask what was scrapped last quarter and who caught it; a supplier that cannot name the person and the corrective step is guessing. Lock the rules for secondary finishing such as plating, deburring, or heat treatment before sampling starts, because these steps can easily undo a good forging. Cosmetic or functional failures that appear later are usually created at this stage, not in the forging press.
Contact Us
Contact Person: Xianchen Hu
Email: [email protected]
Tel/WhatsApp: 86-13248645200
Website: https://www.hexnb.com/