Iron Casting Company Guide: Choosing a Reliable Foundry Partner
2026-11-16
Choosing the right iron casting partner is about more than price per pound—it’s about trust, consistency, and engineering support that holds up under real production pressure. If you’ve ever dealt with late deliveries, porous castings, or a foundry that goes quiet after the quote, you know the difference a dependable supplier makes. In this guide, we break down what separates a reliable foundry from a costly gamble, and why teams looking for long-term stability often turn to Supreme Machinery when the stakes are high.
Pouring line observations that reveal more than a polished pitch
Watch the way a liquid leaves the bottle and the story changes. A slow, uneven break at the lip, a thin stream that clings too long to the glass, or a faint separation in the pour often says more about formulation and handling than any rehearsed benefit list. These small irregularities show up before the first sip, and they are hard to hide with neat packaging or confident wording.
The line itself, where the liquid meets air, can expose viscosity, carbonation, temperature, even storage mistakes. A clean pour with steady color and a soft, even collar usually reflects care earlier in the process. When the stream wobbles or the head collapses quickly, it is not a flaw to ignore; it is evidence of how the product behaves away from a controlled demo.
That is why watching a pour beats listening to a script. Real observations come from repeated, unscripted moments at the counter or the line, not from a slide deck. The details are small, but they accumulate into a clearer picture of whether the product can hold up when no one is smoothing the edges.
Matching iron grades to the actual wear, load, and machining demands
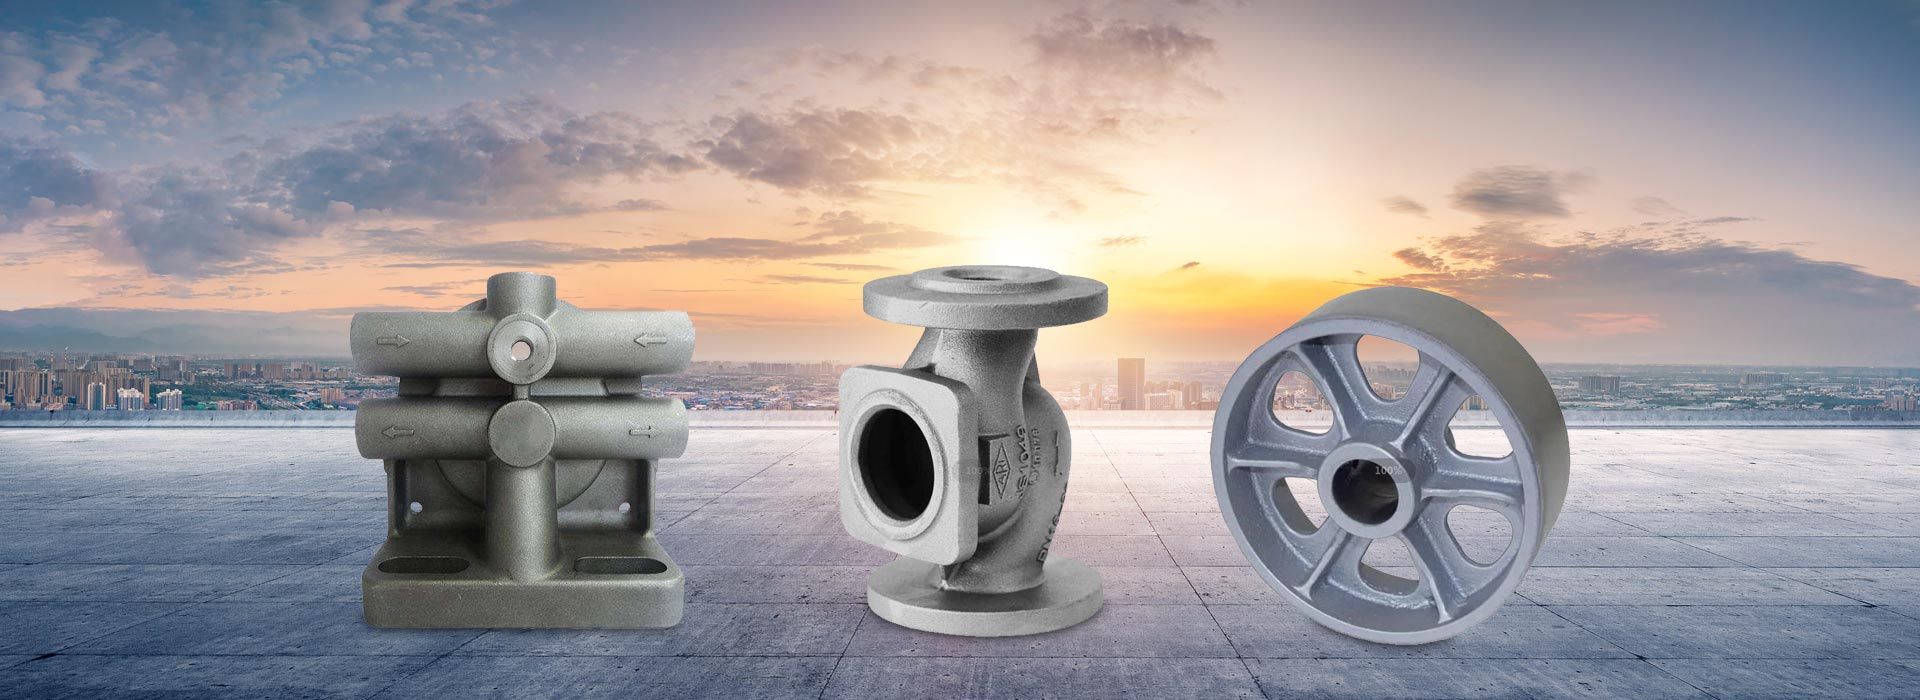
Selecting an iron grade rarely starts with a single alloy number. It starts with the wear surface itself. In sliding or fretting contacts, the graphite in gray iron often does more to control scuffing than a modest increase in hardness ever will, so a pearlitic gray iron with a controlled flake size may outperform a harder but less forgiving alloy. Where abrasive particles dominate, the picture shifts toward martensitic white irons or high-chromium grades, but those choices immediately narrow the machining window.
Load path matters just as much as load magnitude. A heavily loaded bracket that sees occasional shock needs ductile iron because the nodular graphite stops small cracks from spreading the way flakes do. If cyclic stress is the main issue, a pearlitic ductile iron or an austempered ductile iron can carry more stress, though both demand more from cutting tools. Compacted graphite iron sits between gray and ductile when the goal is to raise stiffness and thermal fatigue resistance without accepting the full cost and complexity of a high-nodule casting.
Machining cost often decides whether a theoretically ideal grade stays in the drawing. High carbon equivalent improves chip breaking and reduces tool wear, but it lowers tensile strength and can produce shrink-related defects in thick sections. Small additions of chromium, copper, or tin may stabilize pearlite and raise strength, yet the same elements can create hard carbides at the casting skin. A practical selection therefore sets a hardness band and a microstructure target, not merely a tensile number, and it favors grades that reach those properties through cooling control rather than heavy alloying.
Tooling ownership and hidden costs inside a casting quote
Tooling on a casting quote tends to look like a simple line item, but the real cost depends on who actually ends up owning the die, pattern, or fixture. Some foundries keep tooling title even after you pay the quoted amount, which means that tool becomes their leverage if you try to move work or negotiate a price later. If the quote does not state that ownership transfers to you once the balance clears, ask before the order goes in.
A second layer of cost hides in the conditions attached to the tool. Setup scrap, first-piece trials, dimensional layouts, and spare cavity work may be called out as extras or buried in small print. When tooling is amortized into a per-piece price, the assumed volume matters more than the headline number; run below that volume and you are still covering the full tool cost, while running above it often leaves the supplier holding a margin you never asked about.
The most awkward discussions happen later. Tool repairs, engineering changes, storage, and maintenance reserve fees usually appear after the quote is accepted, often with no cap. If the supplier owns the tool, they also control future production scheduling and minimum order terms. Lock down transfer language, removal rights, and who pays for modifications at the quoting stage so the final invoice does not surprise you.
Batch-to-batch consistency as the real test of a foundry
A foundry can send a perfect first article and still fail the moment production volumes rise. What separates a dependable supplier from a one-time performer is whether the tenth pour, the fifty-third heat, or the third month of machining stays within the same narrow window as the original approval sample. Small drifts in alloy composition, cooling rates, or surface preparation often go unnoticed until a downstream customer sees leaks, cracks, or poor fit.
That repeatability rarely comes from final inspection alone. It lives in how raw material lots are qualified, how worn tooling is tracked, and how operators handle shift handovers. A foundry that quietly logs every variable and adjusts before a parameter drifts too far will produce castings or components that feel boringly identical from order to order, which is exactly what buyers should want.
The real test usually arrives with a reorder placed months later. If the new batch machines, finishes, and performs like the previous one without the buyer asking for special adjustments, the foundry has passed. If the chemistry or dimensions require conversation and compromise, the relationship is still in the sampling phase no matter how many purchase orders have been issued.
Production scheduling proof behind every promised delivery date
Every promised delivery date starts with a current read of the production floor, not a standard lead time pulled from a table. Planners review live queue depth, material availability, and the hours already committed to open orders before a date is ever shared with a customer.
Once an order enters the schedule, it gets a specific slot tied to available equipment and shift capacity. If a machine goes down or an incoming material slips, the schedule is rebalanced the same day. The delivery date is either protected through overtime or adjusted with a clear reason rather than left to drift.
The date on the confirmation is the same working schedule used by production leads each morning. We can usually show the routing, the runtime estimate, and the buffer behind a promise if you want to see how the date was calculated.
Questions a capable iron foundry asks before quoting a job
Most foundries start with the obvious: material grade, quantity, and the drawing. A capable one keeps digging. They ask what the part actually does, how it sits in the assembly, and which surfaces really matter. That changes riser placement, parting line location, and whether a small design tweak could cut porosity risk without changing function. If a foundry quotes from the drawing alone, you are probably talking to a shop that plans to learn on your castings.
The next round of questions usually covers machining stock, tolerances, and testing. Not just what the customer needs, but where the tight dimensions actually land after shrink and stress relief. A strong foundry will ask about leak testing, pressure requirements, surface finish, and whether the customer has a preferred inspection method. They also want to know about annual volume and release schedules, because tooling and pattern decisions that look fine for 50 pieces make no sense at 5,000.
Then there are the less polite questions. Can the part be modified slightly to improve castability? Who owns the pattern, and what happens if the design changes after first articles? What are the rejection limits for gas porosity, sand inclusions, or weld repair? A foundry that asks these before quoting is not being difficult. It is protecting both sides from a contract built on vague assumptions.
FAQ
Ask to see furnace log sheets, spectrometer calibration records, and whether they keep an in-house metallography lab. A foundry that can show inoculation records, chill tests, and microstructure photos from its own lab is managing the melt rather than relying on luck.
Request the last three months of production schedules, key equipment utilization rates, and sand lab results. A dependable operation will share this without hesitation. If you receive only a glossy brochure and a promise, treat that as a capacity risk.
Common ones include excessive machining stock, sand inclusion defects that only appear after rough cutting, unstable hardness that shortens tool life, and delayed containment sorting at your facility. These costs rarely appear in the piece price but dominate the total acquisition cost.
The difference usually comes from trace element control, pearlite-to-ferrite balance, nitrogen levels, and the presence of carbides or slag inclusions. Two shops can both meet the same tensile specification while producing castings with very different machinability.
Ask how they approach pattern strategy for prototype quantities, whether they use soft tooling or printed patterns, and how many times they have successfully moved a part from manual molding to an automated line. Their answers should show a clear handoff process rather than a vague assurance that scaling is easy.
Request process capability data for critical dimensions, quarterly internal scrap rates by defect category, and hardness or microstructure distribution from at least three production batches of a similar part. Real consistency shows up in the spread of those results, not in a certificate on the wall.
Ownership determines who controls modifications, who pays for storage and maintenance, and how easy it is to move the work if the relationship sours. A clear agreement up front prevents the pattern from becoming an expensive hostage later.
When the lower price comes with wider dimensional variation, hidden internal rejections, more machining scrap, extra sorting labor, or unreliable delivery that forces premium freight. The real metric is cost per conforming part installed, not cost per casting shipped.
Conclusion
Choosing an iron casting supplier rarely comes down to the cleanest brochure or the smoothest sales call. A more useful move is to spend time on the pouring line itself, watching how metal is prepared, transferred, and poured. Small things like slag handling, temperature checks, sand compaction, and how quickly molds are closed tell you whether the operation is controlled or just looks busy. Beyond the shop floor, the right iron grade has to match the real demands of the part, including abrasive wear, impact loading, thermal cycling, and heavy machining. A foundry that only asks for a drawing and a quantity may be guessing. The better ones ask about failure modes, surface finish, hardness limits, and how the casting will be fixtured during machining. The conversation around tooling also deserves more attention than it usually gets. Patterns and core boxes carry ownership, maintenance, modification, and storage costs that often sit outside the headline piece price. If those terms are not stated plainly early on, the quote can be quietly incomplete.
Batch-to-batch consistency is where many foundries prove themselves or fall apart. It is not enough that the first sample machines well; the tenth, fiftieth, and five-hundredth pour should behave the same way. Ask for melt records, spectrometer checks, and process logs tied to heat numbers rather than accepting a general assurance. Delivery promises also need evidence. A foundry should be able to show a real production schedule, identify bottleneck operations, and explain how your order fits into existing capacity. If every date is described as no problem without looking at a planner, that confidence is usually borrowed. Pay attention to what the foundry asks before quoting too. Capable suppliers probe application conditions, tolerances, inspection requirements, and past casting failures. A quick quote can feel efficient, but in iron casting it often means the hard questions will come later, after the tooling is cut and the first batch arrives.
Contact Us
Contact Person: Paul
Email: [email protected]
Tel/WhatsApp: 8615067447509
Website: https://www.spironcasting.com