OEM Anodizing Equipment Built for Consistent High-Quality Finishes
2026-10-13
Getting consistent anodized finishes at OEM scale isn't about luck — it's about controlling every variable from rectifier ripple to tank chemistry. Yet too many lines still struggle with shade drift, uneven film thickness, and rework that quietly eats into margins. That's the problem Junda anodizing equipment was built to solve. In this post, we'll look at the design choices that turn a basic anodizing line into a repeatable, high-quality finishing system — and why OEMs are paying closer attention to the equipment behind the finish.
Precision Rectifiers Keep Film Thickness Within Microns
On a roll-to-roll coater running at 200 meters per minute, the gap between the coating head and the substrate drifts by only a few microns—but that is enough to shift film thickness out of spec. A precision rectifier is often the circuit that keeps the loop stable. It takes the raw AC signal from an eddy-current or capacitive displacement probe, strips away the carrier, and delivers a clean DC voltage that corresponds to actual gap distance. Without that clean DC level, the deposition controller would chase noise instead of correcting real thickness changes.
The trick is in the front end. Using a low-bias-current op amp with a pair of Schottky diodes in the feedback path creates an active half-wave or full-wave rectifier that has almost no forward-voltage drop error. Millivolt-level probe signals get linear treatment, so a 1 mV change at the sensor maps to a predictable change at the controller input. Designers often add a second stage with a Bessel filter to kill high-frequency ripple without adding phase lag, which matters when the coating line changes speed quickly.
One line making capacitor film switched to this approach after drifting out of tolerance during afternoon shifts when temperatures rose. The previous diode-bridge circuit needed recalibration twice per shift; the precision rectifier has held thickness variation at ±0.4 microns across a 12-hour run. The real test came with a sudden substrate splice—the rectifier's fast settling time let the coater pull the gap back before the splice mark reached the winding station. That is not a specification on a data sheet; it is why operators keep requesting it.
Tank Lining Materials That Resist Acid Attack for Years
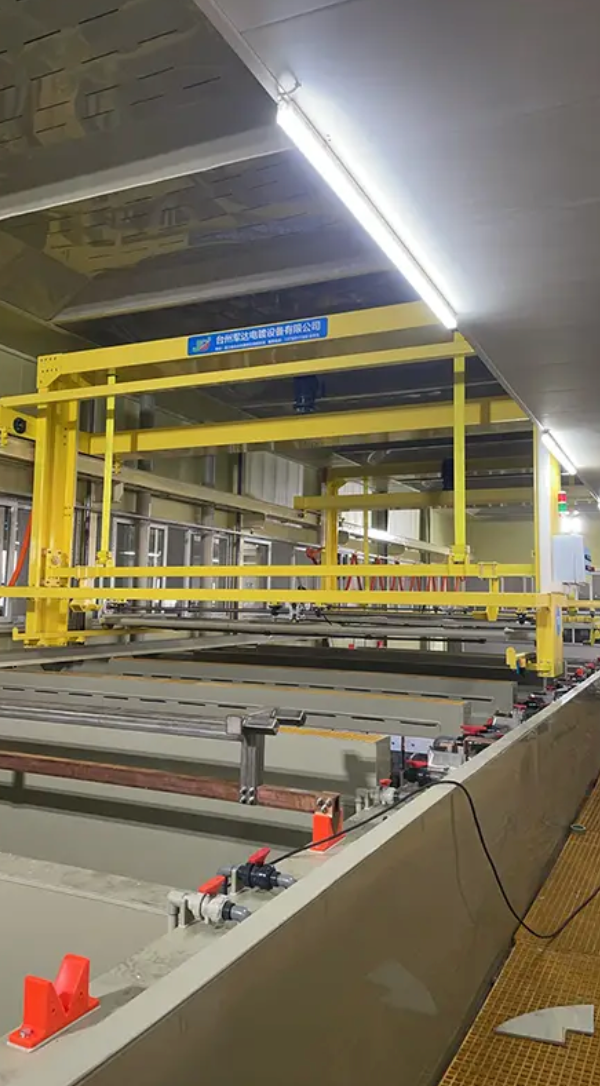
Selecting the right tank lining for acid storage goes far beyond picking a generic chemical-resistant coating. The most dependable systems rely on materials that form a tight, low-porosity barrier, such as fluoropolymer linings, which shrug off sulfuric, hydrochloric, and nitric acid even at elevated temperatures. Unlike thin paint-like coatings, these linings are often installed as thick sheet membranes or spray-applied layers that cure into a seamless, flexible shield. Over years of exposure, they resist cracking, blistering, and under-film corrosion, which are the usual failure points in aggressive acid service.
Rubber linings, particularly those based on bromobutyl or chlorobutyl formulations, also deliver long-term acid resistance when correctly vulcanized to the steel substrate. Their resilience allows them to absorb minor tank flexing and thermal cycling without losing adhesion. For highly concentrated acids or mixed chemical streams, dual-layer systems—such as a chemical-resistant thermoplastic bonded over an elastomeric base—provide an extra margin. The key is not just the polymer chemistry but the installation quality: hand-welded seams, spark testing for pinholes, and proper surface preparation determine whether a lining will last two years or twenty.
In practice, facilities that document lining thickness, hardness, and adhesion after curing, and then inspect annually, get dramatically longer service life from the same base material. Ceramic-filled epoxy systems and glass-flake reinforced vinyl esters can also withstand acid attack, but they demand meticulous application to avoid weak spots at welds and nozzle penetrations. For decades of reliable service, engineers increasingly pair acid-resistant linings with cathodic protection and periodic ultrasonic thickness monitoring, turning what was once a routine maintenance headache into a low-risk, long-cycle asset.
Agitation Flow Patterns That Prevent Air Pockets and Streaks
In many mixing vessels, the difference between a flawless finish and a surface riddled with defects comes down to how the fluid moves. Simple vortex-style agitation looks impressive but often drags air down the shaft, creating pockets that later emerge as pinholes or cloudy streaks. A far more effective pattern uses a combination of low-shear axial flow near the top and gentle radial mixing at the bottom, keeping the surface in constant slow rotation without breaking it. This keeps air from being entrained while still moving denser components off the bottom.
The placement of baffles and the shape of the impeller play a bigger role than many operators realize. Instead of relying on a single high-speed blade, a staggered configuration with a downward-pumping hydrofoil can generate a rising central column that collapses outward at the liquid surface. That outward surface flow acts like a natural skimmer, pushing any trapped micro-bubbles toward the vessel wall where they dissipate rather than being pulled back into the bulk. For high-viscosity fluids, a slow helical ribbon agitator works even better—its continuous wiping motion prevents stagnant zones where air films cling and later streak through the product.
Small adjustments to speed and direction can also break up repeated flow paths that lead to consistent streaking. Running the agitator in a timed reversing cycle, even for a few seconds every couple of minutes, disturbs the established laminar channels and redistributes any microscopic air pockets before they coalesce. In many production environments, this simple change reduced visible streaking by more than half without any new hardware, simply because the fluid no longer followed the same worn-in path over and over.
Modular OEM Frames Adapt to Changing Part Geometries
Standard machine frames rarely keep pace with the realities of modern production. A fixture built for one part quickly becomes dead weight when that part changes. Modular OEM frames eliminate this waste by letting you reconfigure the base structure just as often as the part geometry demands. Swap in longer rails, reposition cross members, or add an extension without scrapping the core assembly.
The real advantage shows up in mixed-volume shops. Instead of ordering a bespoke frame for every new workpiece, you start with a common chassis and adjust only the points that matter—clamp locations, support heights, or clearance zones. This keeps changeover time low and prevents the frame itself from becoming the bottleneck. The hardware is designed to be taken apart and reassembled without losing alignment, so the same base can serve both a short, wide casting and a long, narrow extrusion.
Over the life of a project, this adaptability reduces the total number of frames you need to stock. You stop treating the frame as a permanent monument to one design and start seeing it as a reusable platform. When the next part revision lands, the frame bends with the change instead of breaking the budget.
Closed-Loop Cooling Keeps Electrolyte Temperature Stable
In a closed-loop cooling setup, the electrolyte never comes into direct contact with the cooling medium. A dedicated circuit pumps a coolant—often a water-glycol mixture—through a heat exchanger that sits adjacent to the electrolyte reservoir or flow path. Heat transfers across the exchanger walls, and the warmed coolant then passes through a radiator or chiller before returning. Because the loop is sealed, there’s no evaporation, no contamination, and no need to top up fluid levels during normal operation.
The system responds to real-time temperature readings from sensors placed in the electrolyte stream. When the temperature drifts above a set threshold, the coolant flow rate increases or the chiller kicks in to pull heat out faster. If the electrolyte cools too much, the loop can bypass the chiller or reduce flow, allowing the electrochemical process itself to bring the temperature back into range. This narrow-band control matters because electrolyte conductivity, viscosity, and reaction kinetics are all temperature-sensitive.
Compared to open-loop or passive cooling methods, a closed-loop design keeps the electrolyte chemically unchanged. There’s no ingress of dust, moisture, or oxygen that could degrade the solution over time. It also eliminates the risk of external water mixing with the electrolyte, which can happen in open evaporative systems. For long-duration operation, that stability translates into more predictable performance and fewer maintenance interruptions.
Automated Hoist Scheduling Preserves Finish Consistency at Scale
In high-volume finishing lines, manual hoist scheduling often creates subtle drift in dwell times and transfer sequences. Operators chase throughput, occasionally shortening or lengthening process steps to keep the line moving. That variability shows up as color shifts, uneven coating thickness, or inconsistent surface treatment across identical parts. Automated scheduling removes this guesswork by locking hoist movements to a deterministic model that respects every tank’s required immersion window. The result is a finish that repeats batch after batch, even as the line scales from dozens to thousands of units per shift.
What makes automation different isn’t just speed—it’s the ability to hold finish-critical parameters stable when upstream flow fluctuates. A well-tuned scheduling engine anticipates load changes, reroutes hoists around bottlenecks, and still returns each carrier to the same station at the same point in the process envelope. Operators who once made judgment calls every few minutes now monitor exceptions only. That shift reduces rework, cuts chemical waste from over-processing, and keeps line capacity predictable. At scale, the cumulative effect is a finish consistency that manual methods simply can’t sustain.
FAQ
We focus on fluid dynamics first—each tank has an eductor-based agitation loop that keeps electrolyte temperature and concentration uniform within ±0.5°C across the whole bath. The rectifier is pulse-capable with tight ripple control, so the oxide layer grows evenly even on complex shapes.
The cathode placement and tank geometry are modeled for each line, not just copied from a template. We use auxiliary cathodes and adjustable air sparging to pull current into recesses, minimizing the shadow effect you see with standard setups.
Yes—automated bath sampling and dosing keep pH and aluminum concentration stable, and the cooling system uses a plate heat exchanger sized for the actual rectifier output, not the tank volume, so temperature drift stays under 1°C during continuous runs.
It’s fairly low. We spec non-shedding tank liners and bolt-on anode/cathode rails that can be swapped in under 20 minutes. The filtration is cartridge-based with differential pressure indicators, so operators change elements before quality drops, not after.
We routinely meet MIL-A-8625 Type II and Type III, as well as automotive and architectural specs. The line includes an integrated CCD thickness gauge and a conductivity-based sealing bath monitor, so you get real-time pass/fail instead of lab lag time.
We use a two-stage ramp profile—low current density for the first few minutes to establish a uniform barrier layer, then switch to the main anodizing current. Fixtures are custom machined from titanium with spring-loaded contacts to avoid hot spots.
Yes, the rectifier and heat exchanger are sized with a 40% turndown range, so you can run one small rack or a full load without changing the chemistry behavior. The PLC stores recipes per part number, making changeover under ten minutes.
For a standard 5-stage line (clean, etch, desmut, anodize, seal) with a 4-foot tank width, we can fit it in about 1,200 square feet including rectifier and scrubber space. We also offer modular expansion if you later add hard coat or dyeing.
Conclusion
Achieving uniform anodized finishes across high-mix production starts with equipment that removes guesswork from the process. Precision rectifiers hold current density within tight limits, so film thickness stays within microns even on complex profiles, while low ripple output prevents localized overgrowth at edges and corners. Tank linings engineered from chemically resistant materials shrug off years of acid exposure, eliminating the contamination and uneven etching that degrade surface quality. In the bath itself, carefully directed agitation flow prevents stagnant zones where air pockets or streaks would otherwise form, ensuring every face of the part sees the same electrochemical conditions.
Beyond the tank, modular OEM frames allow quick reconfiguration when part geometries shift, so the line does not become a bottleneck for new product introductions. Closed-loop cooling keeps electrolyte temperature from drifting, which matters because even a few degrees of change alters pore structure and final color consistency. At scale, automated hoist scheduling coordinates dwell times and transfer speeds across multiple tanks, removing the variability that manual handling introduces. Rather than treating these as isolated upgrades, an OEM approach integrates them into one control architecture, so operators see real-time deviations instead of reacting after defects appear. Together these elements create a repeatable anodizing system where first-article results match production runs, batch after batch.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com