Turnkey Complete Cleanrooms Company: Simplifying Controlled Environment Projects from Design to Certification
2026-09-13
When a cleanroom project starts to feel like a juggling act between designers, contractors, and certification bodies, you lose time, money, and focus. That's where a true turnkey approach changes everything. At GENO Pharmatech, we've built our reputation on simplifying controlled environment projects from the first sketch to final certification—no handoffs, no finger-pointing, just one accountable partner.
Why Your Cleanroom Project Needs Fewer Cooks in the Kitchen
Cleanroom builds live or die on precision, and every extra voice in the planning phase adds friction that the final environment can’t afford. When too many contractors, consultants, or internal stakeholders weigh in without a single clear owner, details like airflow patterns, material compatibility, and protocol sequencing get diluted. The result isn’t better oversight—it’s a patchwork of compromises that shows up later as delayed validations or costly rework.
A tighter team doesn’t mean fewer skills; it means fewer handoffs. One lead who understands both the regulatory stakes and the physical build can make consistent calls without re-litigating decisions. That focus keeps documentation clean, change orders rare, and the project’s tolerances intact from design freeze through final certification.
Blueprints, Build-Out, and Beyond: One Company Chases the Details
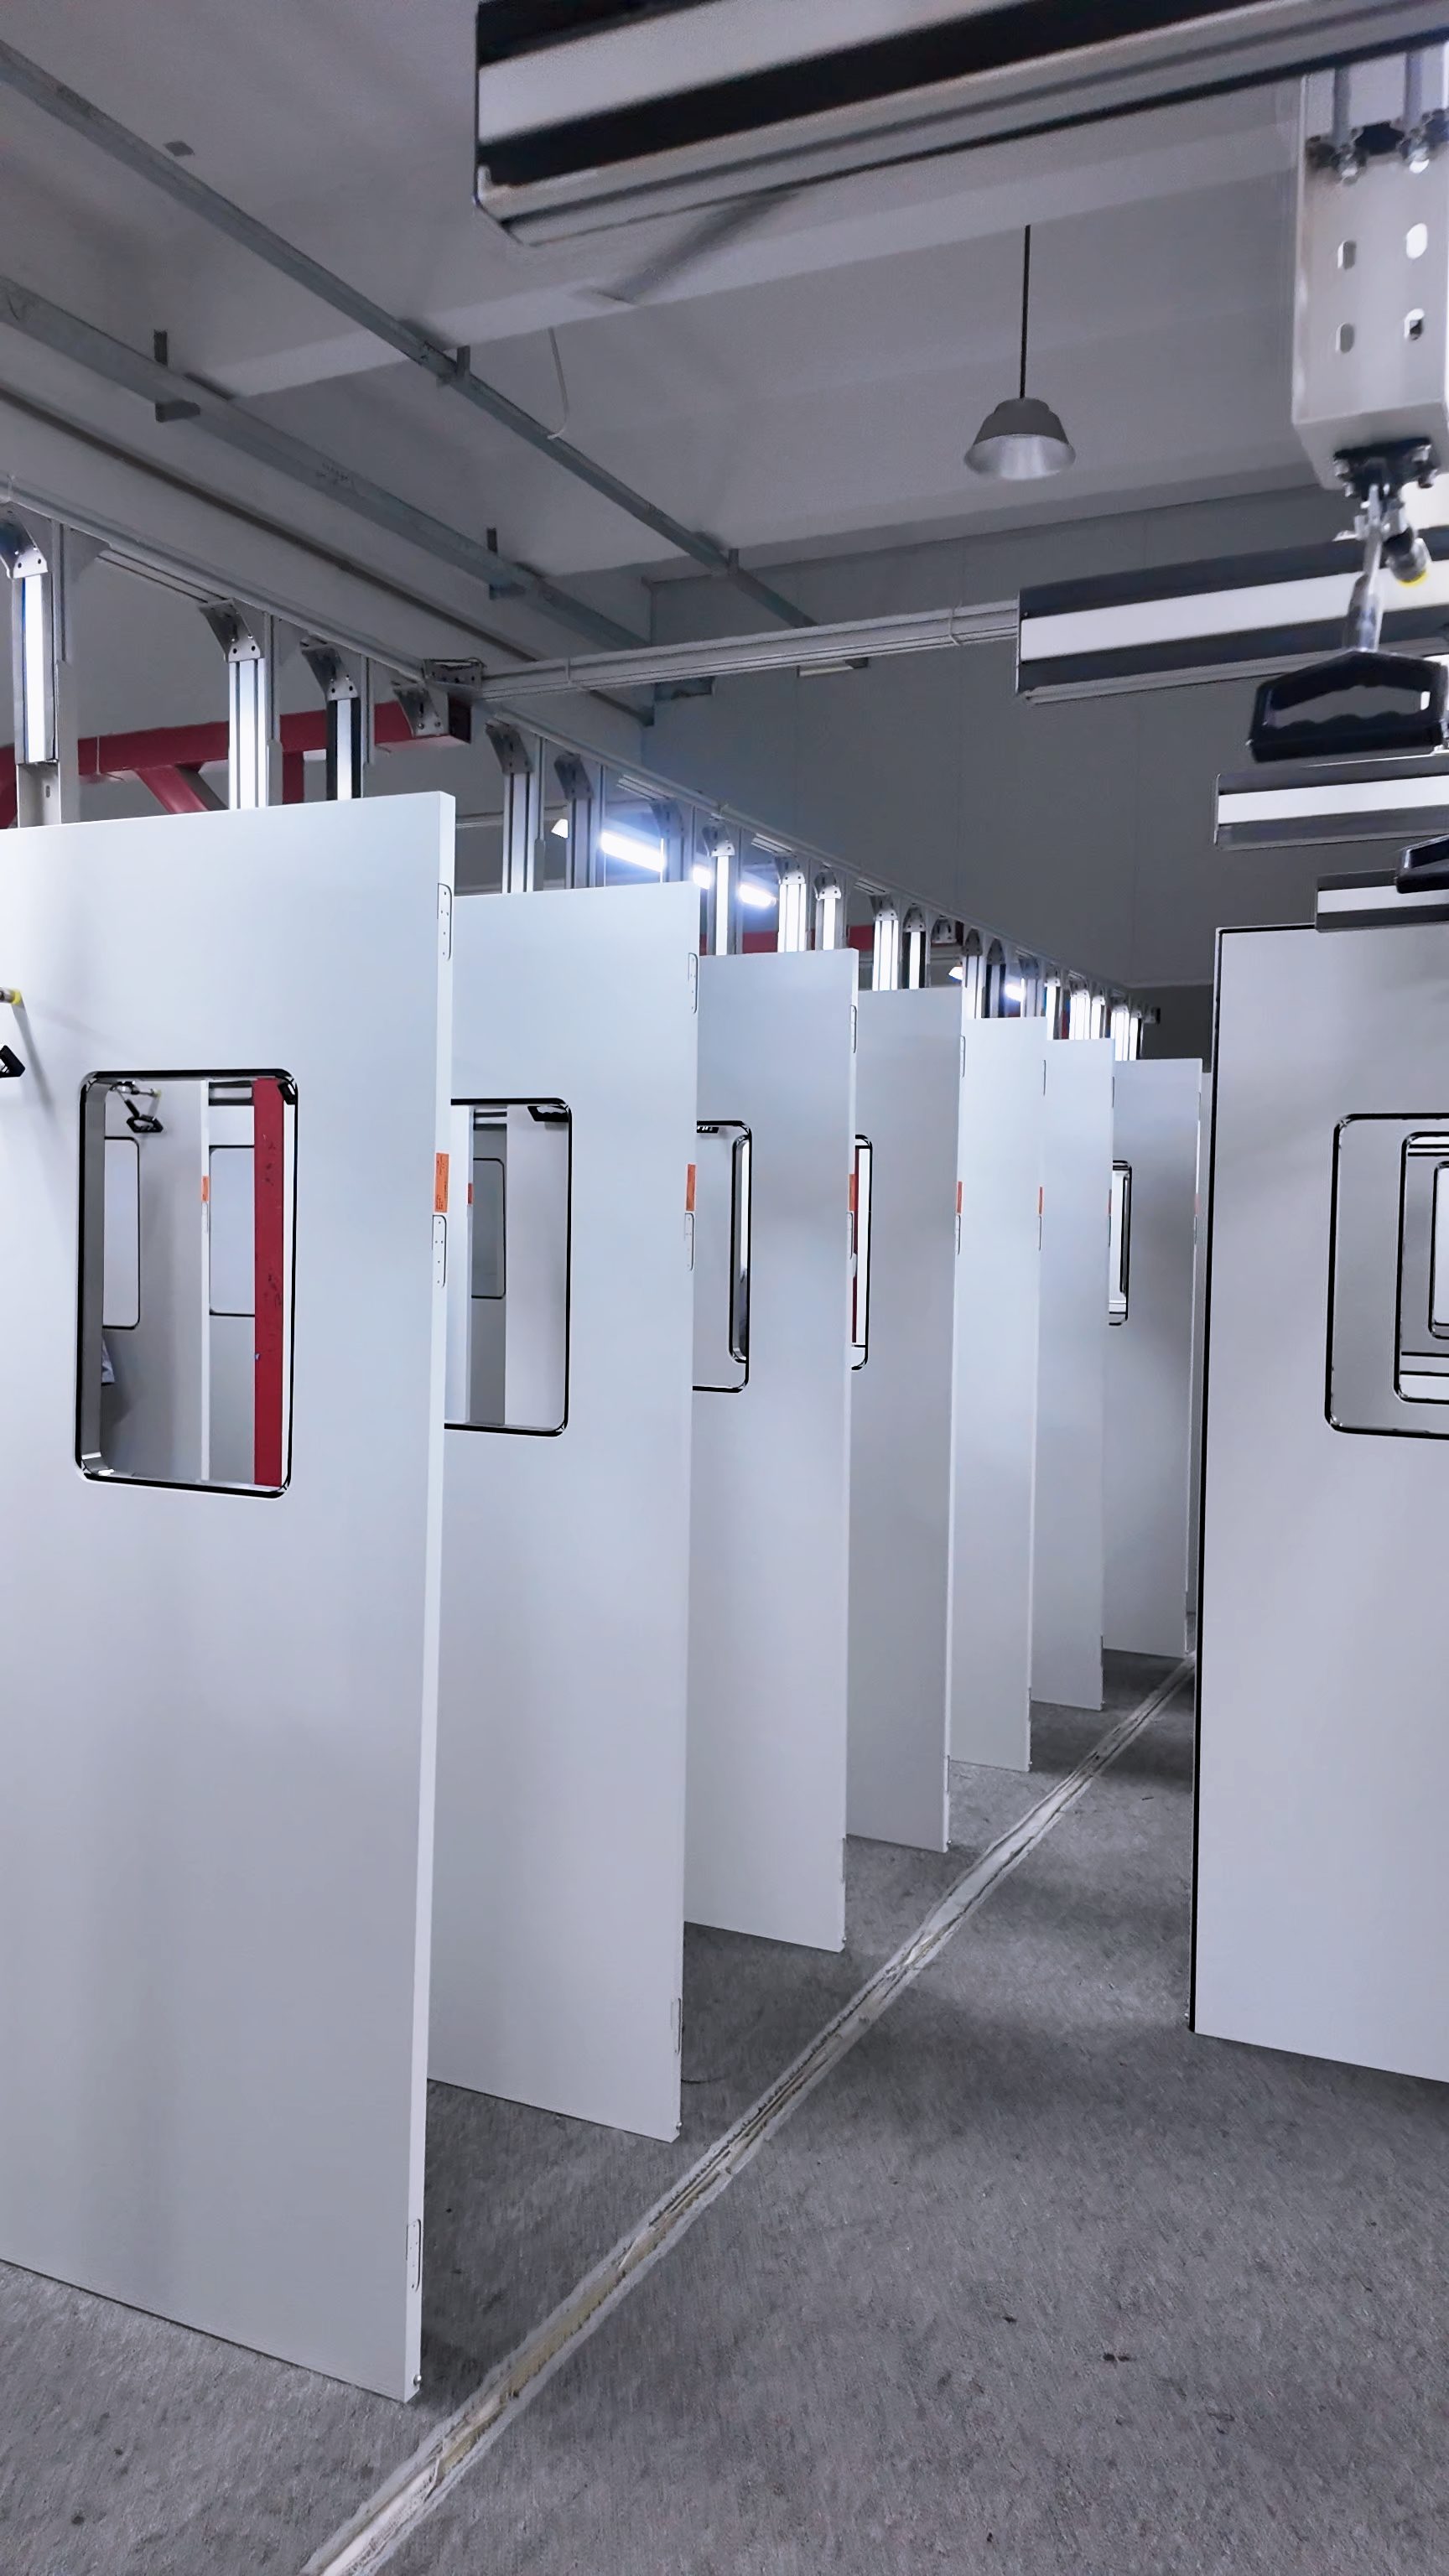
In the back office of a midsize construction firm in Ohio, the blueprints aren't just rolled up and forgotten. They're annotated in three colors of ink, dog-eared at the corners, and occasionally spread across a conference table long after the project has broken ground. One project manager keeps a running list of every change order, not because the client demanded it, but because she noticed that the original door swing on the second-floor bathroom would clip the towel rack. When the framing crew arrived, the detail was already baked into the revised drawings. That's the rhythm here: small fixes caught early, passed down the line without fanfare.
The build-out phase is where those quiet decisions start to show up in steel and drywall. Walk through a half-finished office shell and you'll see it in the alignment of electrical boxes with window mullions, or in the way the HVAC vents are tucked just behind a bulkhead so the ceiling grid stays clean. A site supervisor doesn't carry a punch list on his phone; he carries a pocket notebook with pencil sketches of the places where the subcontractors tend to cut corners. He'll circle a gap in the fire caulking, then stand there for ten minutes explaining to the drywall crew why it matters for sound isolation, not just code. The drywallers roll their eyes, but the next day the caulk is neat and continuous.
Beyond the handover, the company keeps chasing details that most builders would call finished. Six months after a restaurant opened, the original project team came back to check a recurring draft near the patio door. They found a missing weatherstrip that had slipped through the final walkthrough, replaced it, and then spent an afternoon adjusting the door closer so it wouldn't slam. The chef never asked them to do it. The owner never noticed the original problem. But the people who built the place remembered the way the light hit that doorway in the renderings, and they wanted the real thing to feel just as intentional.
The Turnkey Cleanroom That Puts Compliance on Autopilot
Most cleanroom projects stall at the handoff—too many vendors, mismatched specifications, and a pile of documentation nobody has time to reconcile. This turnkey approach removes that friction entirely. You are not handed a shell and told to figure out the rest. Instead, the room arrives fully integrated: walls, filtration, HVAC, monitoring, and controls are already talking to each other before the first validation run.
Compliance becomes a byproduct of the design rather than a monthly scramble. Sensor data feeds directly into audit-ready reports, pressure cascades hold steady without manual tweaking, and alarm thresholds are set to the exact limits your process requires. The system flags drift early, so a small adjustment never turns into a batch rejection or a regulatory finding.
What makes it feel effortless is the quiet consistency. Operators do not need to become cleanroom engineers. They walk in, follow the on-screen status, and trust that the environment is where it should be. That reliability lets your team focus on what they actually make, not on babysitting the room that makes it possible.
From First Sketch to Final Certification: Zero Loose Ends
Every line on the initial drawing sets a commitment in motion. We treat that first sketch not as a rough idea, but as the opening sentence of a contract with precision. Each revision, each material choice, each tolerance call gets logged against a master checklist that nobody is allowed to bypass. When something feels ambiguous, we pause and resolve it on the spot—because a loose thread at the concept stage becomes a knot at the certification stage.
Moving from prototype to production, the same obsession follows. Test failures aren't hidden in footnotes; they're dissected in front of the whole team. A bracket that vibrates loose, a seal that weeps under thermal cycling, a connector that fits only after force—these become design changes, not excuses. The documentation stays alive, updated with every tweak, so there is no gap between what we built and what we claim we built.
By the time the final certification audit begins, the trail is complete. Drawings match parts, parts match test reports, test reports match the original requirements. An auditor can trace any dimension back to the sketch that started it, and forward to the torque wrench that verified it. That is what zero loose ends means to us: not a slogan, but a habit of closing every loop before it has a chance to unravel.
A Controlled Environment Without the Usual Finger-Pointing
When a project slips or a system breaks, the instinct in many teams is to find a name to attach to the failure. That reflex rarely fixes anything, but it's deeply human. A controlled environment strips away that reflex by making it clear from the first minute that no single person will be put on the stand. Instead, the room focuses on the sequence of events, the decisions made with the information available at the time, and the gaps that allowed a small error to turn into a larger one. The difference is immediate: shoulders drop, voices steady, and people start volunteering details they would otherwise hide.
Practical changes support this shift. Meetings begin with a simple reminder that the goal is to improve the system, not to grade individuals. Timelines are reconstructed on a whiteboard, with each step labelled as fact, assumption, or unknown. If someone says "I thought the API was already updated," that statement isn't used to assign blame but to trace where the assumption came from and why it wasn't verified. This approach exposes weak points in documentation, handoffs, and communication patterns without making anyone feel attacked. People learn that admitting a mistake early makes the whole group smarter, not more vulnerable.
Over time, the absence of finger-pointing becomes self-reinforcing. Teams start to treat incidents as puzzles rather than court cases. New members observe that being wrong in this room is safe, and they mimic that openness. The result is not a soft or timid culture; it's a sharper one, where problems surface faster and fixes stick because they address the real conditions that produced the failure. That kind of clarity only comes when people stop worrying about who will be blamed next.
The Cleanroom Build That Treats Certification as a Starting Point
Most cleanroom projects treat the final ISO certification as the finish line—pass the particle count, sign the paperwork, and hand over the keys. This build flips that logic. From the first architectural sketch, the team assumed certification was merely the lowest rung. The real target was a facility that would stay within spec even when filters aged, gowning protocols slipped, or production schedules pushed airflow to its limits.
That mindset changed material choices and layout. Instead of sealing every gap and hoping for the best, the designers ran redundant HEPA banks, oversized recirculation loops, and pressure cascades with enough headroom to absorb real-world chaos. Even the door interlocks and pass-through chambers were specified to support future retrofits—because in five years, the cleanest room is the one that can adapt without ripping out walls.
After certification, the team kept the particle counters running and tied the data into the building management system. A drift of just a few microns per cubic meter triggers maintenance alerts long before limits are breached. Certification was a starting point, not a trophy. That's the difference between a cleanroom that passes a test and one that keeps the product safe every single shift.
FAQ
From our side, turnkey means you hand us the requirements and we take care of everything else—layout, mechanical design, construction, qualification, and final certification. You don't have to coordinate multiple vendors or chase down missing pieces.
We use a single point of contact and a phased schedule that covers design reviews, material selection, installation, and testing. That way you always know what's happening next and what decisions are needed from your side.
We work with ISO 5 through ISO 8 cleanrooms, including modular hardwall and softwall systems, for industries like pharmaceutical, semiconductor, medical device, and research labs.
Certification is included in our turnkey scope. We perform the required testing—particle counts, airflow, pressure differentials—and provide documentation that meets ISO 14644 or other applicable standards.
Yes, most projects are retrofits. We do a site survey to understand your available space, utility connections, and traffic flow, then design a layout that makes sense without major disruption.
We build flexibility into the schedule and use modular components where possible. If you need to add a pass-through, change a gowning area, or adjust pressure cascades mid-project, we'll assess the impact and give you a clear cost and timeline update before proceeding.
It depends on size and classification, but a small to mid-size modular cleanroom often runs 8 to 14 weeks from design approval to certification. We'll give you a realistic timeline after the initial consultation.
We don't disappear after handover. We can provide maintenance contracts, recalibration schedules, and help with re-certification when your cleanroom's operational window expires.
Conclusion
Most cleanroom projects stall because too many vendors own too few pieces of the puzzle. One firm handles the architectural drawings, another chases the mechanical contractor, and a third only shows up after the walls are up. Turnkey Complete Cleanrooms removes that chaos by keeping a single accountable team on the project from the first napkin sketch to the final certification report. Fewer cooks in the kitchen means the design intent survives untouched. The same engineers who draft the blueprints also manage the build-out, so pressure differentials, airflow paths, and finish details are not lost in translation. It is a quieter, faster way to get a controlled environment that actually meets spec.
That continuity also changes what completion means. Instead of handing over keys and hoping the certifier agrees, the turnkey team treats certification as the starting line, not the finish. Compliance is baked into daily construction decisions, not bolted on after a failed test. When one company owns the details—from HEPA placement to door sweep clearance—there is no finger-pointing between architect, builder, and cleanroom certifier. Zero loose ends means the final walkthrough is not a negotiation; it is a formality. The result is a cleanroom that operates as designed on day one, with documentation that proves it, and a client who never has to referee the usual vendor blame game.
Contact Us
Contact Person: Amy Yang
Email: [email protected]
Tel/WhatsApp: 008619330882686
Website: https://www.genopharmatech.com/